IN Brief:
- Two UK frozen-food lines were modernised over an 18-month project while production disruption was managed.
- The installation incorporates more than 150 variable-speed drives, at least 16 motor control centre sections and over 40 remote nodes.
- The control architecture uses ControlLogix PLCs, FactoryTalk View interfaces and EtherNet/IP to coordinate equipment from multiple suppliers.
Actemium UK has completed an automation and control systems upgrade across two high-capacity frozen food production lines at an unnamed UK manufacturing site. The 18-month project replaced ageing controls and linked equipment from multiple suppliers, addressing recurring stoppages, restricted fault information and limited visibility of operating performance.
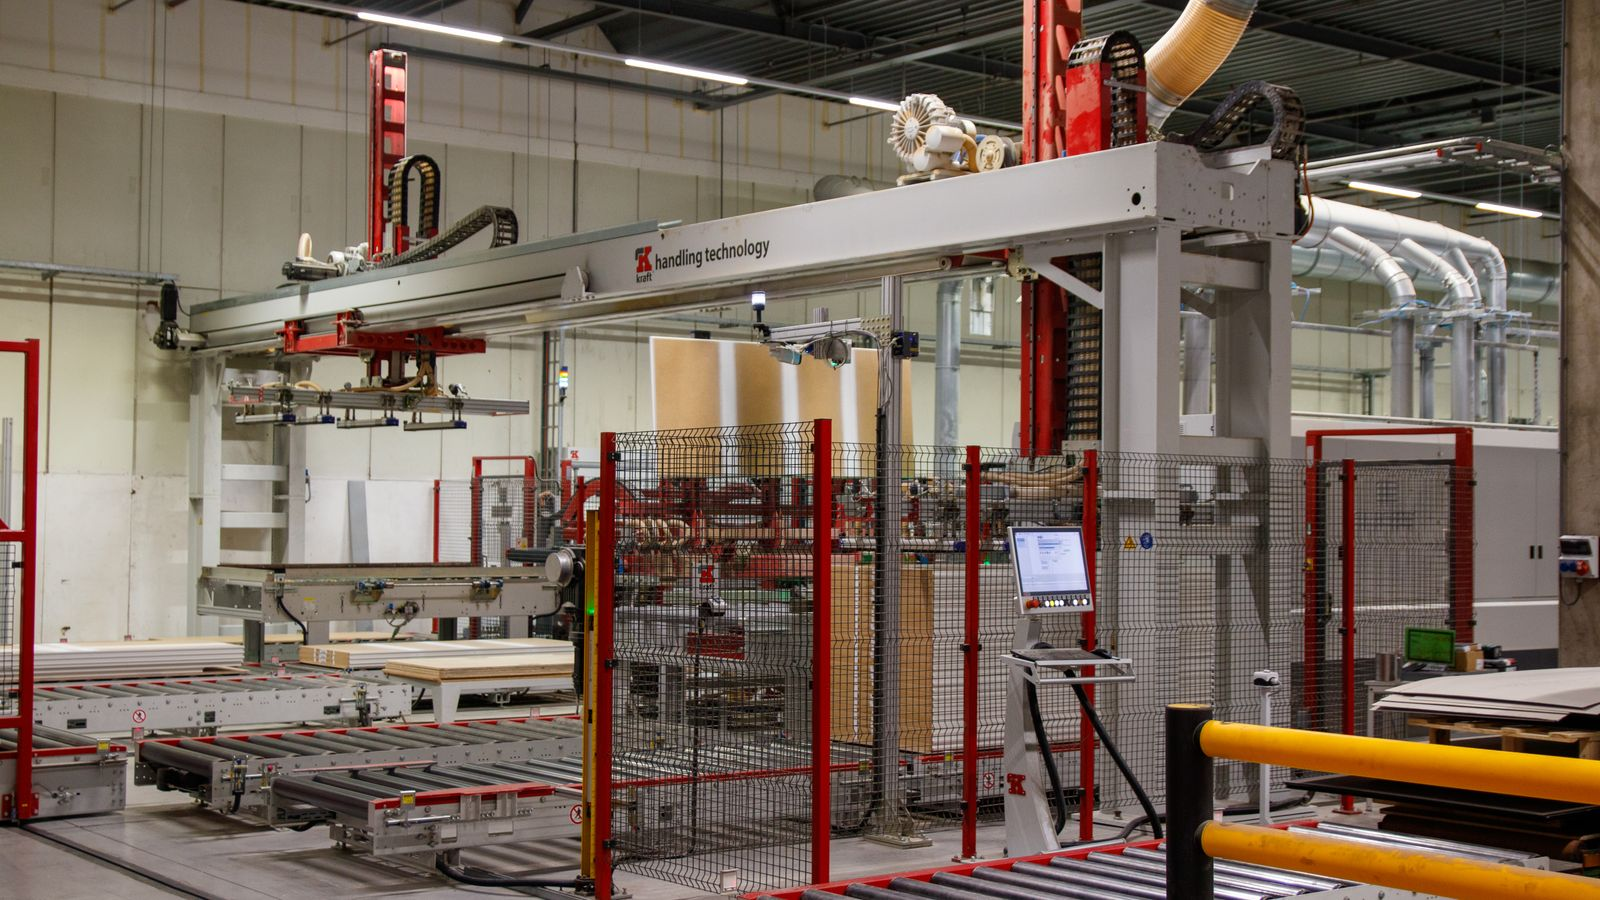
The lines operate at a reported finished product throughput of 15–25 tonnes per hour. Their combined modernisation involved more than 150 variable-speed drives, at least 16 motor control centre sections and over 40 remote control nodes. Equipment from more than six specialist suppliers was integrated on each line, covering stages from raw material intake to transfer into cold storage.
Actemium Automation Peterborough delivered the work from engineering design and control-panel manufacture through software development, testing, installation and commissioning. The customer has not been named. The upgrade was arranged around continuing production, with controls for machinery from more than six suppliers on each line brought into a common operating sequence rather than replaced as isolated pieces of plant.
The upgraded architecture uses Rockwell Automation ControlLogix programmable logic controllers to coordinate the line, with FactoryTalk View human-machine interfaces for operator control and monitoring. EtherNet/IP provides industrial network communications among the main control systems and connected equipment. Distributed input/output hardware and managed switches link field devices to the control platform and improve the information available when a fault occurs.
The drive installation includes Rockwell PowerFlex 525 and ABB equipment. Variable-speed drives adjust motor speeds electronically, allowing conveyors and other driven machinery to be coordinated rather than running at fixed rates regardless of changing process conditions. In a line involving washing, preparation, cooking, freezing and packaging, inconsistent transfers between stages can accumulate products, interrupt flow or leave downstream equipment starved of material.
Actemium’s integration work covered sequencing, recipe management, changeovers and safety interlocks, so a downstream machine’s state could be considered before an upstream conveyor continued feeding product. Automated start-up and shutdown sequences reduce some manual interventions, while the operator screens bring process status and alarms together. Synchronised running conditions are especially important when a cooking stage feeds a freezing stage that cannot absorb unlimited fluctuations in product flow.
Condensation and low temperatures also affect the reliability of sensors and other electrical equipment in frozen-food production. The project involved equipment running through washing, preparation, cooking, freezing and cold storage transfer, with different environmental conditions along the route. Actemium identifies these operating constraints but has not disclosed the site’s product temperature set points, line-specific loss rates or measured changes in energy use.
The modernisation also addressed a maintenance problem created by fragmented controls. Where equipment from separate vendors operates in sequence, a stoppage can originate in one machine but appear as a fault several stages away. First-out fault identification, event logs and maintenance notifications now give engineering staff more information about where an interruption began. Networked drive diagnostics also support remote checks of operating conditions.
Production monitoring incorporates overall equipment effectiveness information, throughput reporting, downtime analysis and historical data. Those tools allow the operator to compare actual running conditions with the planned production sequence and to identify recurring restrictions. Actemium reports improved operational visibility but has not released measured before-and-after figures for overall equipment effectiveness, downtime or waste reduction.
Keeping both lines available during the transition required detailed installation planning. Control panels and software were tested before delivery through factory acceptance procedures, allowing interface and logic problems to be resolved away from the production floor. Site work then included electrical checks, network validation, drive commissioning and safety verification. The commissioning sequence moved from dry running to tests with product before normal production ramp-up.
Operator training accompanied the handover of the new controls and diagnostics. Maintenance teams now have access to alarm histories, event information and networked drive diagnostics that can help isolate a fault before restarting equipment in the appropriate sequence. The replacement of ageing components also gives the manufacturer a platform designed for future modifications, with spare network capacity and control software intended to accommodate further expansion.
The final commissioning phase moved from testing without product to live product runs and then production ramp-up. Actemium reports stronger reliability, consistency and visibility following the modernisation, but has not published numerical before-and-after results for downtime, factory output or waste. The documented throughput range and hardware counts establish the scale of the engineering work; any percentage improvement would require comparable production data from the manufacturer.