IN Brief:
- Well-Fed has opened expanded ready-meal production facilities in Shotton, Flintshire.
- The site is expected to process up to 500 tonnes of surplus food each year.
- Reusable metal trays are intended to reduce reliance on single-use plastic meal packaging.
Well-Fed has opened an expanded ready-meal production facility in Shotton, Flintshire, designed to turn surplus ingredients into affordable prepared food at greater scale. The development has received support from the Welsh Government, The National Lottery Community Fund and Moondance Foundation, and is expected to process up to 500 tonnes of surplus food annually.
The food manufacturing and distribution service grew out of work involving Can Cook, ClwydAlyn Housing Association and Flintshire County Council. Well-Fed has operated in North Wales since 2019, using recoverable ingredients to produce nutritionally assessed meals for households and community partners. Its commercial kitchen and meal services were already established in Shotton before the expansion, which increases the space and systems available for production. The changing mix of available surplus ingredients will continue to influence production planning and menu availability.
More than one million fresh meals have been supplied since the service began, according to Well-Fed. Its portfolio comprises over 140 nutritionally assessed meal options, although that represents the broader range rather than the number produced on any one day. The organisation employs 24 people, including 18 who were previously unemployed. Director Robbie Davison expects the expanded facility to support further production, employment and distribution across Wales as volumes develop. The expansion also includes a plan to replace up to 160,000 single-use plastic trays with reusable metal trays over two years.
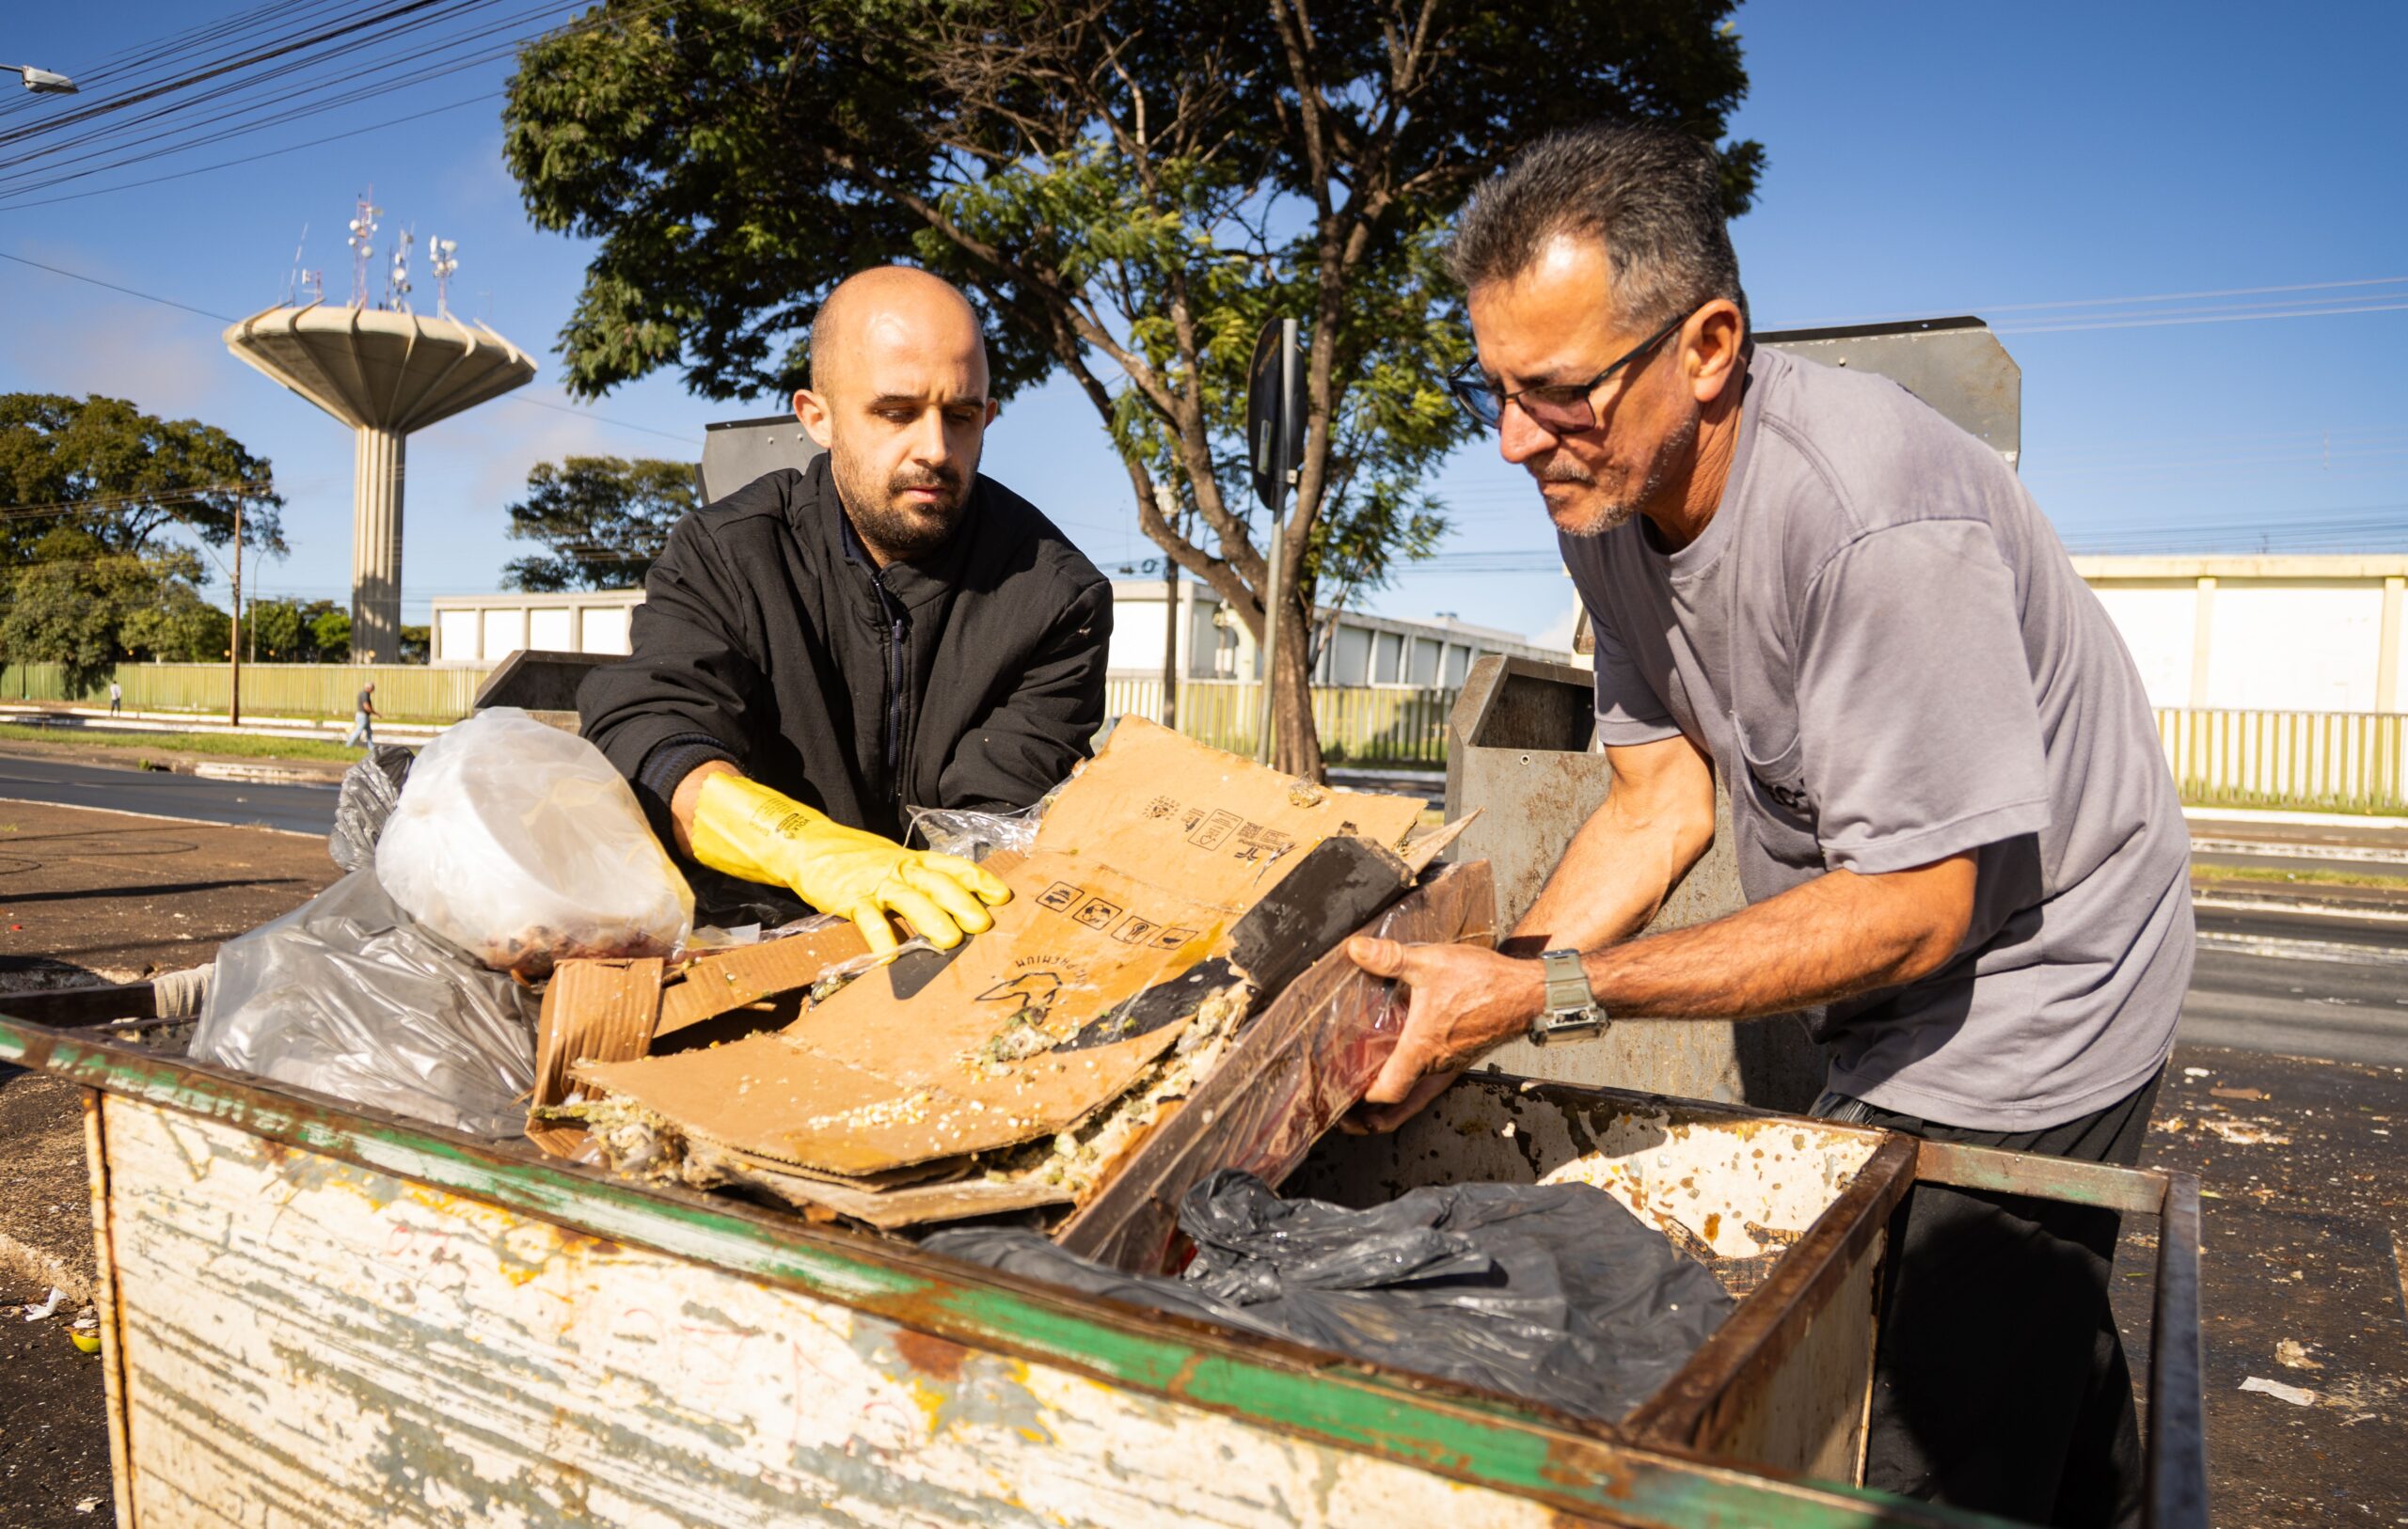
Processing surplus ingredients at the planned scale requires regular intake, assessment and storage of variable raw materials. Ingredient suitability depends on condition, temperature history and remaining shelf life at receipt. Food accepted for production can then be allocated to recipes and batches with appropriate traceability, handling and segregation controls.
Surplus food arrives in less predictable quantities and varieties than ingredients purchased against a fixed production specification. Batch planning consequently has to accommodate changing stock while maintaining defined recipes, allergen information, nutrition, traceability and finished-product quality. Additional factory capacity creates room to handle more material, provided those operating controls scale with throughput.
Ready-meal production involves preparation, cooking, chilling and packing operations, each with its own capacity and food safety controls. Increasing batch numbers requires those stages to remain aligned, particularly where meals must be cooled and held at appropriate temperatures before distribution. The Shotton investment adds production capability to Well-Fed’s existing chilled-meal service.
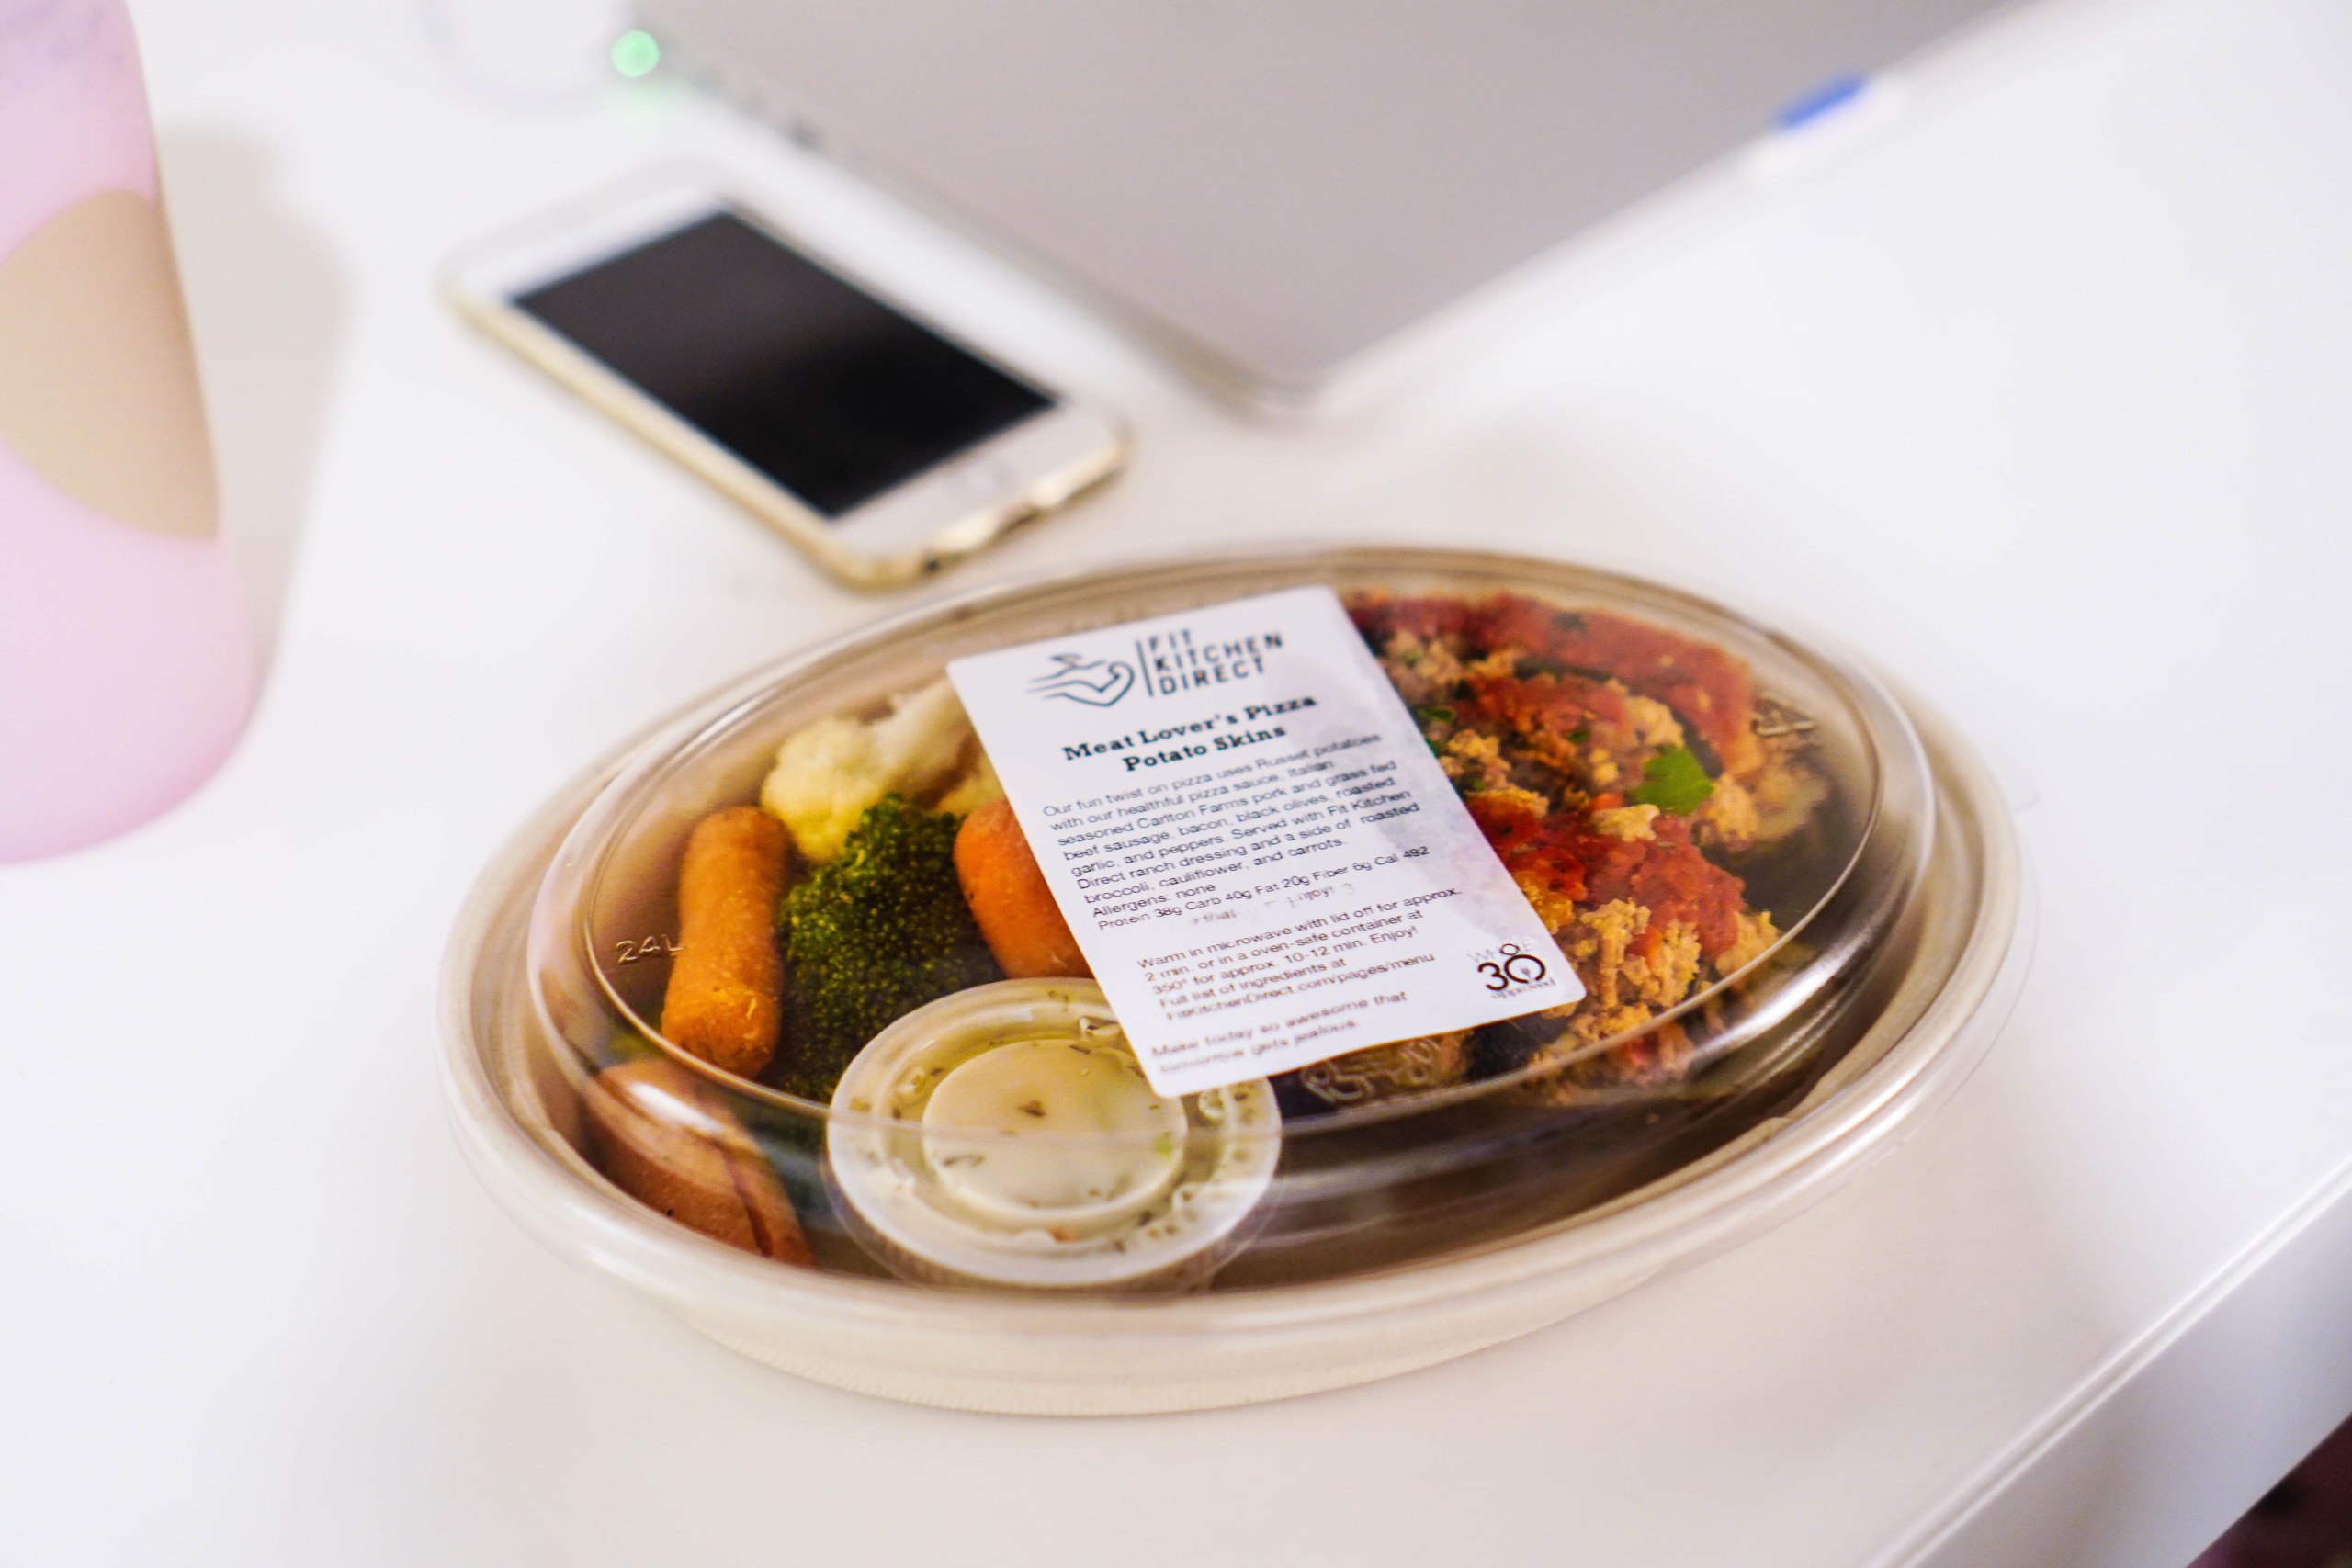
Well-Fed already supplies chilled microwave-ready meals, recipe bags and slow-cooker packs across Flintshire, with a rotating menu. Its distribution model includes direct deliveries and community collection points. Earlier this year, refrigerated food lockers were installed beside St Asaph Cathedral, allowing orders to be collected independently of staffed opening hours while products remain chilled.
Refrigerated collection points and direct deliveries make chilled storage and dispatch part of the production plan. Finished meals have to move through an appropriate temperature-controlled chain, with production schedules aligned to the collection windows and capacity of lockers and delivery vehicles. Higher output therefore requires matching packing capacity, dispatch arrangements and control over the time between production and collection.
Reusable metal meal trays change how packaging moves through the Shotton operation. Unlike disposable packs, containers need to be collected after meals have been distributed, cleaned to an appropriate hygienic standard, checked for damage and returned to the packing process. The anticipated reduction in plastic packaging remains a future target, dependent on sufficient trays completing repeated cycles.
Enough clean trays must be available for new batches while filled or used containers remain with customers, at collection points or in transit. The number required in circulation depends on the frequency of deliveries, return rates and the time spent washing and inspecting trays. Those variables affect packing continuity as well as the practical balance between packaging avoided and the resources used to recover it.
Returns from community outlets and customers will need to be coordinated with deliveries of chilled meals. Damaged or missing trays must be replaced without disrupting packing, while returned equipment needs to be kept separate from clean stock until it is ready for food contact. This makes tray recovery part of the distribution and sanitation operation, with its own inventory and handling requirements.
Incoming surplus ingredients must be assessed while there is still enough shelf life for preparation, cooking, chilling and dispatch. Staff then have to allocate suitable materials to viable recipes and complete batches before that window narrows. Receiving capacity and chilled storage can restrict the volume recovered even when the kitchen itself has spare production capacity.
As output rises, dispatch capacity and refrigerated storage must keep pace with the meals leaving the production line. A larger kitchen can recover more suitable ingredients only if receiving, batch preparation, chilling, packing and delivery operate in sequence without creating backlogs. Coordinating those stages will determine how much additional surplus food is converted into safe, consistently prepared meals and how reliably those meals reach households and community collection points.