IN Brief:
- Samworth Brothers was fined £594,000 after two workers were scalded during steam-pipe maintenance at Kettleby Foods.
- HSE found failures in risk assessment, safe-working procedures, isolation, lock-off, supervision and work-at-height controls.
- The case demonstrates the engineering and management controls required before intrusive maintenance begins on food-factory utilities.
Samworth Brothers has been fined £594,000 after two workers suffered serious scald injuries while carrying out maintenance on steam pipework at its Kettleby Foods factory in Melton Mowbray.
An employee and a contractor were replacing a leaking gasket in an isolation valve in the boiler room when hot water escaped from the pipework. One worker suffered subdermal burns affecting around 4–5% of the body, while the second sustained second-degree subdermal burns over approximately 9%.
The men had been working from a gantry above the boiler, but the access platform did not reach the section of pipework requiring repair. Both therefore stepped away from the gantry and worked directly on top of the boiler before the gasket was removed.
An investigation by the Health and Safety Executive found that the task had not been adequately risk assessed and that Samworth Brothers had not documented a safe system of work for the activity. Suitable isolation and lock-off procedures were not used, while the work at height was undertaken without sufficient measures to prevent a fall.
HSE also identified inadequate supervision and monitoring to ensure the expected procedures were followed. Samworth Brothers pleaded guilty to breaching Section 2 of the Health and Safety at Work etc. Act 1974.
Birmingham Magistrates’ Court imposed the £594,000 fine on 4 September, together with £5,834 in prosecution costs and a £2,000 victim surcharge. The company was also ordered to pay £6,000 compensation to the injured employee.
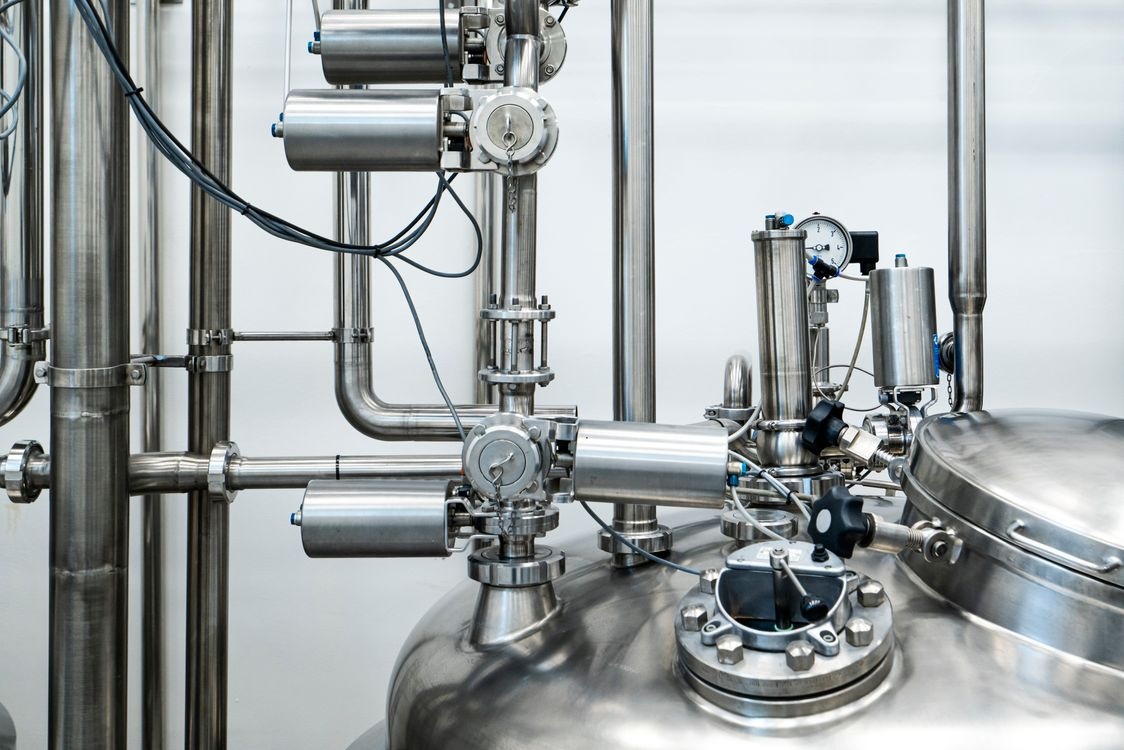
The circumstances involve equipment familiar to almost every large food factory. Boilers, steam distribution, hot-water systems, refrigeration and compressed-air networks support production continuously, but maintenance on those utilities can expose engineering teams to stored energy long after individual production machines have stopped.
Steam and hot-water systems require particular care because closing a valve does not by itself prove that downstream pipework is safe to open. Residual pressure, trapped condensate, thermal energy, leakage and incorrect valve position all have to be considered before a flange, gasket or other component is disturbed.
A formal isolation procedure therefore has to do more than identify the nearest shut-off point. Every relevant energy source needs to be established, isolations secured against inadvertent operation and the integrity of those isolations verified before intrusive work begins.
HSE guidance links that process with job documentation including risk assessments, method statements, permits and isolation certificates. Those controls establish how the work should proceed, who has responsibility for proving the plant safe and what has to be checked before the equipment is returned to service.
The access arrangement at Kettleby Foods added a separate hazard. Once the workers had to leave the gantry to reach the valve, the job was no longer being performed from the position for which the access equipment had been provided.
Maintenance planning has to recognise that change before work starts. Temporary platforms, scaffolding or other appropriate access equipment may be necessary even where the engineering repair itself is relatively modest.
Food factories can make those decisions more difficult because maintenance windows are often short. A boiler or steam-system fault may affect cooking, cleaning, hot water or several production areas simultaneously, creating pressure to restore services quickly before throughput and customer orders are affected.
The commercial urgency does not reduce the energy contained within the system. Short interventions place a greater premium on preparation because suitable access, replacement parts, permits and isolation points have to be ready before the plant is opened.
The involvement of both an employee and a contractor also shows why maintenance controls have to cross organisational boundaries. Contractors may bring specialist engineering skills, but the site operator controls the factory and understands how the utility network interacts with production and other services.
A permit-to-work system provides one mechanism for coordinating those responsibilities, although the document itself is only useful if physical conditions match what has been recorded. An isolation certificate cannot compensate for a valve that has not been secured or a section of pipe that still contains pressure.
Digital maintenance systems can improve planning by linking work orders with equipment history, permits and spare parts, but the final verification remains a physical engineering task. The condition of the plant has to be proved before someone begins dismantling it.
The Kettleby Foods incident arose during a relatively conventional gasket replacement rather than an unusual production process. That makes the prosecution more relevant, not less: ordinary corrective maintenance can carry severe consequences when the controls around energy isolation, access and supervision break down.
Food manufacturers depend on utilities to keep high-throughput sites operating, and maintenance teams are routinely required to intervene when those systems fail. HSE’s prosecution demonstrates the standard expected before that intervention begins — a defined method, effective isolation, suitable access and supervision capable of ensuring the controls are actually followed.